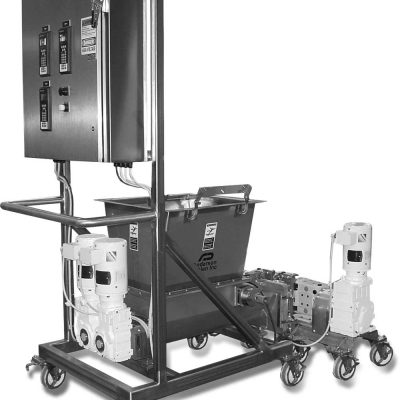
Our custom pump feeders are designed to move high-viscosity products that cannot be moved by gravity or with standard pump equipment. The high-torque, low-RPM, counter-rotating, and synchronized augers enable our feeder systems to transport material and maintain a consistent flow. They’re engineered to connect seamlessly to your existing system, helping deliver better control, efficiency, and a reliable product feed to your operation.
After being installed, the pumps have improved customers’ ergonomics, production, and sanitation across the processing line. These systems are built to operate continuously and meet demanding production needs day after day. The feeder pumps are used in food, pharmaceutical, and chemical industries.
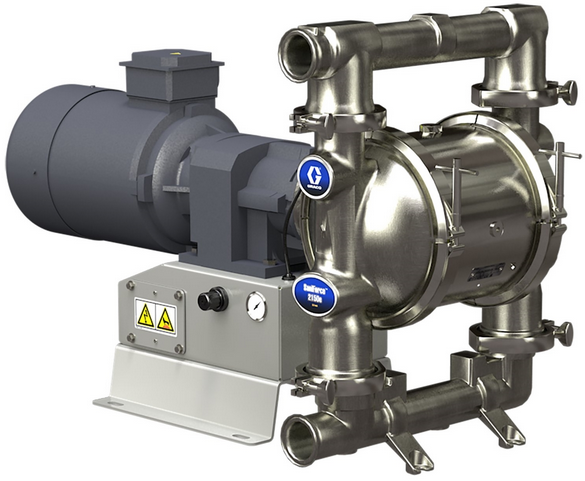
Pump feeders are designed to move thick, high-viscosity products and provide a consistent feed into your processing system. Pairing the feeder with the right sanitary pump maintains reliable product flow while meeting the hygienic requirements of food, beverage, pharmaceutical, and other sanitary applications. Explore our sanitary pump options to find the right solution for your process.
Whether you’re evaluating new equipment or upgrading an existing system, our team can help you learn how a custom pump feeder can support your specific application. Read through our FAQs below, or contact us for additional information or to check specifications.
Pump feeders are used to move high-viscosity products that cannot be effectively transferred by gravity or standard pump equipment. They are commonly used to transport thick, dense, or difficult-to-handle materials within processing environments. These systems help maintain a consistent flow and controlled feed across the production line.
Our pump feeders use high-torque, low-RPM, counter-rotating, synchronized augers to transport material through the system. This design helps move products that may otherwise struggle with conventional pumping methods and ensures reliable, continuous operation.
Our custom pump feeder equipment is used in food, pharmaceutical, and chemical processing applications where a set, controlled movement of high-viscosity products is required. Each application is engineered to meet industry-specific processing needs.
Yes. Pump feeders are designed to provide controlled product movement and consistent feed rates, helping improve production flow, ergonomics, and sanitation within the manufacturing process. They also help reduce manual handling.
Our pump feeders include advanced features that allow you to precisely control feed rates, monitor pump pressure and inlet/outlet conditions, transport products that cannot move with gravity alone, and support temperature-controlled processing applications.
Yes. Our pump feeders can help achieve temperature changes of a few degrees, supporting applications where maintaining product consistency and set processing conditions is important.
Yes. Our custom pump feeders are engineered to meet the application requirements, product characteristics, and operational needs of the process, supporting reliable material transfer and production performance.

Our team is here to answer questions, provide quotes, and offer customer support. Let us know how we can help.